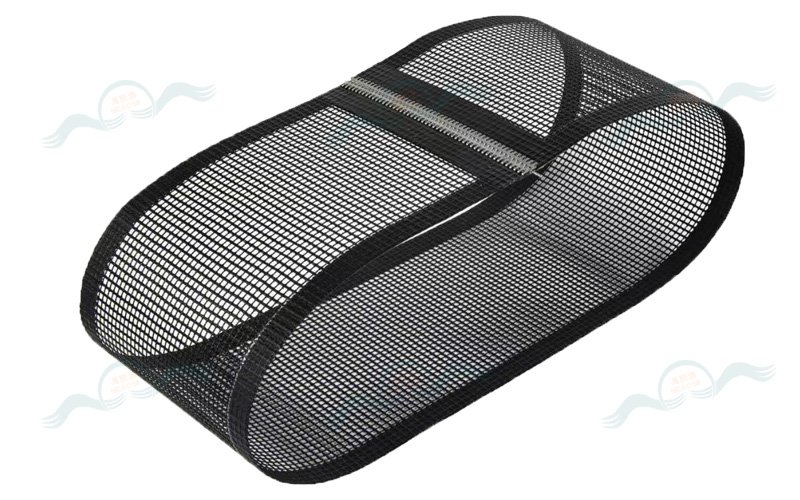
Applications of PTFE Teflon Conveyor Belts
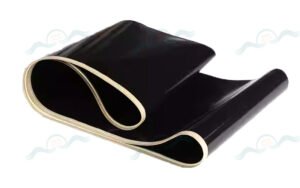
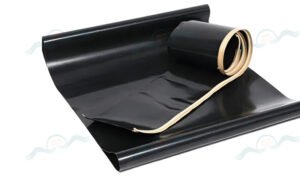
We are a professional manufacturer of all types of PTFE (Teflon) conveyor belts. The outstanding properties of PTFE conveyor belts determine their extremely wide range of applications. The primary application areas are as follows:
1. High and Low Temperature Environments
Due to their exceptional high and low temperature resistance, PTFE conveyor belts can be used in a wide variety of extreme temperature conditions. They exhibit excellent weatherability and aging resistance, suitable for operating environments ranging from a minimum of -196°C to a maximum of 300°C.
In actual service:
- Continuous use at 250°C for 200 days: no reduction in tensile strength whatsoever; no weight loss
- Exposure at 350°C for 120 hours: weight loss of only approximately 0.6%
- At -180°C ultra-low temperatures: original flexibility is fully retained
2. Conveying Sticky & Adhesive Products
The inherent non-stick properties of PTFE conveyor belts result in an extremely smooth surface that is easy to clean. Virtually all adhesive substances — including pastes, resins, and coatings — can be easily removed from the surface. PTFE conveyor belts are therefore ideal for conveying products prone to adhesion, including items contaminated with oil, stains, or other surface deposits.
3. Conveying Chemical Products
PTFE conveyor belts offer outstanding chemical corrosion resistance — capable of withstanding attack from strong acids, strong alkalis, and a wide range of organic solvents. This makes them well-suited for chemical product conveying applications in corrosive industrial environments.
4. Conveying Pharmaceutical Products
PTFE conveyor belts possess excellent chemical resistance and are completely non-toxic — resistant to virtually all pharmaceutical substances and reagents. They are widely used in pharmaceutical manufacturing and drug product conveying applications where material purity and safety are paramount.
5. Conveying Electronic Products
PTFE conveyor belts offer superior electrical insulation performance — with a dielectric constant typically below 0.0025 — combined with UV resistance and anti-static properties. These characteristics make them highly suitable for electronic product conveying applications where electrostatic discharge protection and insulation integrity are critical requirements.