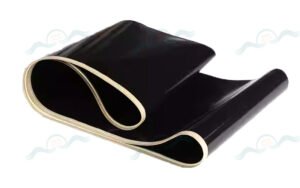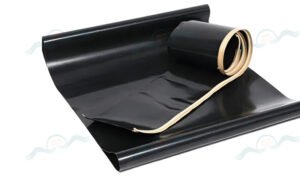
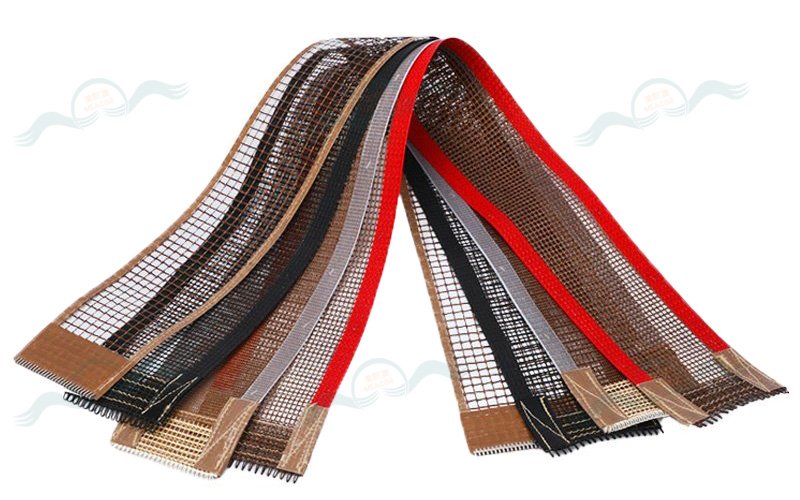
In specialized industrial scenarios such as high-temperature drying, heat sealing, chemical processing, and food dehydration, standard conveyor belting suffers from accelerated aging, thermal deformation, and physical failure due to intense heat and corrosive agents. PTFE conveyor belts serve as high-performance continuous transfer carriers, engineered specifically to withstand extreme thermal and chemical operating environments.
I. Thermal Resilience & Extreme Chemical Stability
- Temperature Endurance: Continuous operation ranges from -60°C to +260°C without structural degradation, withstanding short-term temperature peaks up to 300°C without melting, warping, or cracking.
- Chemical Inertness & Biosafety: Highly resistant to strong acids, alkalis, and organic solvents. The non-toxic, odorless surface meets cleanroom standards for food processing and precision manufacturing.
II. Long Service Life & Anti-Aging Durability
- Operational Longevity: Delivers a standard service life of 2 to 3 years under typical operating conditions.
- Tensile Retention: Maintains original tensile strength and belt weight even after hundreds of days of continuous operation at 200°C, showing superior resistance to thermal fatigue and degradation.
III. Dimensional Specifications & Customization
- Custom Dimensions: Supports fully customized configurations, with standard gauge thicknesses ranging from 0.08 mm to 1.35 mm and maximum widths exceeding 4 meters.
- Versatile Adaptability: Mesh aperture sizes, surface textures, and splice joint styles are fully adaptable to OEM machine frameworks across various budget requirements.